Troubleshooting a Sudden Drop in Plastic Granulator Output: A Practical Guide for Production Managers
Maintaining a steady production rate is the backbone of any profitable plastic manufacturing operation. However, every production supervisor eventually faces that frustrating moment when their high-performance plastic granulator machine suddenly loses its speed and output drops significantly. When your plastic recycling granulator slows down, it directly eats into your daily margins, disrupts your downstream processes, and delays your shipping schedules. Understanding why this happens and knowing exactly how to fix it will save your engineering team hours of costly downtime.
Why Your Plastic Recycling Granulator Loses Throughput
The first step to restoring your hourly production target is identifying the bottleneck within your plastic pelletizing machine. More often than not, a dramatic drop in throughput points to a few common mechanical or thermal disruptions inside the screw and barrel.
One of the most frequent culprits is a severely clogged screen pack. As your plastic recycling granulator processes production waste, factory regrind, or raw polymers, the mesh screens filter out degraded polymers, un-melted additives, and external contaminants. Over time, this debris builds up and creates massive backpressure. This high pressure forces the polymer melt to slow down, drastically reducing the volume of material exiting the die head.
Thermal Issues and Feed Throat Bridging
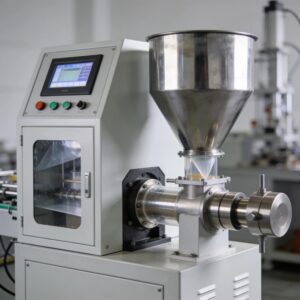
Another common issue is material bridging at the feed throat, which happens when the temperature in the initial feeding zone rises too high. When the raw resin, flakes, or masterbatch softens prematurely right beneath the hopper, it sticks to the feed throat walls and forms a solid block. This block prevents new material from dropping onto the screw, causing the plastic granulator machine to run semi-empty.
Additionally, you must check for broken heating bands along the barrel zones. If a specific heating zone fails, the plastic in that section will not melt completely. The resulting cold spot acts as a physical restriction, creating immense mechanical resistance, spiking your motor current, and slowing the entire extrusion process.
Mechanical Wear Inside the Plastic Pelletizing Machine
Mechanical wear on the internal components also plays a major role in long-term performance loss. If you have been running filled materials, glass fiber compounds, or abrasive resins through your plastic pelletizer equipment for months without an overhaul, the clearance between the screw flights and the barrel wall might have widened. This increased gap allows the molten plastic to flow backward over the flights instead of being pushed forward, resulting in a severe drop in output.
Fixing a sluggish plastic granulator machine requires a systematic approach to cleaning, temperature calibration, and regular hardware inspection by your maintenance team.
Optimizing Filters and Temperature Controls
First, implement a regular schedule for replacing the screen pack based on your backpressure gauges. If your plastic recycling granulator is not equipped with a hydraulic continuous screen changer, you will need to pause production briefly to swap out the blinded screens for fresh mesh. Upgrading to an automatic screen changer can virtually eliminate this specific downtime issue by allowing filters to be swapped without stopping the line.
Next, address the thermal balance at the feed zone to stop material bridging. You need to inspect the cooling water jacket around the feed throat to ensure it is clear of scale and flowing at the correct rate. Lowering the temperature of the feeding section keeps the raw material solid until it is properly engaged by the screw flights.
Restoring Mechanical and Electrical Efficiency
To solve the issue of material backflow, your technicians must regularly measure the clearance between the screw and the barrel of the plastic pelletizing machine. If the wear exceeds the manufacturer’s recommended tolerances, it is time to pull the screw for rebuilding, re-flighting, or complete replacement. Keeping a spare screw in your factory inventory ensures you can swap the parts quickly and avoid weeks of waiting for a custom fabrication.
Finally, perform a quick electrical audit on the heating system. Use a digital multimeter to check the continuity of each heating band along the barrel. Replacing a dead heating ring is a quick, inexpensive fix that immediately restores the thermal profile required for your plastic granulator machine to pump material at its rated capacity. By keeping a close eye on these key areas, you can keep your production line running smoothly and maintain consistent hourly output.